Make inspection part of the workflow
If industrial coating quality control is postponed until the finished surface is examined, much of the relevant evidence may already be hidden. The identity of materials, the prepared substrate, decisions made during application and the component's waiting conditions cannot always be reconstructed reliably afterwards. An inspection plan should therefore guide the work from the beginning rather than become a form completed at the end. Its purpose is not to collect every possible piece of data. It should obtain the information needed at the right time, identify who can release the next operation and show where to look when a problem arises. A consistent component and work-order identity connects incoming materials with the eventual dispatch decision.
Begin with a concise account of the service conditions and delivery expectations. Which surfaces are to be coated, which areas must be protected, what appearance is required and which specification governs acceptance? Resolve these questions before selecting from the industrial coatings range. A product routinely used on one line is not automatically suitable for another component. Technical, production and purchasing staff need to see the same scope. For each operation, identify the responsible person, inspection timing, governing document, required record and route for dealing with a nonconformity. A signed form cannot compensate for an undefined acceptance criterion or an unclear authority to proceed. The plan must support real decisions during production.
Connect specifications, product documents and samples
A project may involve a customer specification, drawings, an approved colour sample, product data sheets and safety documentation. Each answers a different question. Approval of a sample's appearance does not define application conditions, and a product data sheet does not necessarily cover every contractual delivery requirement. The plan should show which document governs each subject. If information conflicts, the operator should use an established technical decision route rather than choose whichever instruction seems easier to follow. Record the applicable revision and date. A superseded printout left at a workstation is a simple example of why document access belongs in the inspection plan. The right information must be available to the people who actually perform the work.
Describe different coating functions on separate lines, such as an epoxy primer and an epoxy topcoat. The local technical catalogue archive identifies their different roles, while current application values should be confirmed for the product being supplied. Copying a ratio or drying time from a generic online table is not a suitable way to populate a work order. A reference field can reduce the risk of the same value being copied into several documents and drifting out of alignment. The published steelwork coating system specification guide offers related planning context. Such references help organise the work; they do not replace the technical approval required for a particular project.
Treat material receipt as more than a quantity check
At receipt, establish whether the delivered material matches the purchase requirement. Check product and component identities, batch information on the containers, quantity, visible package condition and the required documents. Receiving the base component of a two-component system does not mean that the complete set is available for application. Keep incomplete or uncertain material distinguishable from material released for use. Warehouse receipt and technical release can be separate decisions, so that accepting a delivery is not confused with approving its contents for production. Record damaged packaging, unreadable labels or unexpected products and refer them to the responsible person. Similar names must not become an undocumented basis for treating different products as equivalents.
Storage organisation should make the correct selection easier without replacing product identification. For example, quick-drying industrial primer and quick-drying industrial topcoat have distinct roles, regardless of where their containers sit on a shelf. Check storage and usability conditions against the applicable documents. Using the oldest delivery first is not the entire decision; the material must still be valid and approved for the job. Link an issue from stores to the relevant work order. Partly used containers need an identifiable status and a decision about further use. Do not release a container with an uncertain history merely to avoid interrupting production. A clear hold status is preferable to a guess.
Preserve component identity through preparation
Correct identification of the component is as important as correct identification of the coating. Similar-looking parts can have different surface requirements, masking details or delivery classifications. Plan a marking method that remains usable through preparation and painting, including how identity will be transferred if the original mark must be removed. The operator should be able to recognise areas that must remain uncoated from the applicable drawing. A form carrying only a general product name may allow different drawing revisions to be treated as the same job. Component number, drawing revision and work-order reference reduce that ambiguity. If a production batch is split and later brought together, keep the links between each subgroup and its processing records.
Before preparation starts, determine whether the component is ready to enter the coating process. Incomplete fabrication, inaccessible details, unresolved findings or uncertain surface information should not be passed forward as though the preceding work were complete. Where a shop primer is already present, confirm its status in the intended subsequent system. Its name alone does not determine every later operation. The published edge and weld inspection planning article offers further context for those details. Fabrication acceptance and coating-preparation acceptance may belong to different people. The inspection plan should make clear that completion of one responsibility does not automatically fulfil the other or authorise work outside the agreed scope.
Inspect evidence before it is covered
Do not rely on the final painted appearance to reconstruct the condition of the prepared surface. Define the required preparation method and acceptance criteria beforehand, then complete the relevant inspection before coating begins. Identify hold points that prevent the next operation from starting without release. Their purpose is not to stop production unnecessarily; they protect the opportunity to assess a condition that will later be concealed. If the nominated inspector is unavailable, the route for obtaining alternative authority should be clear and recorded. Preserve the distinction between an informal comment and a technical release. Prepared components in a waiting area must retain their identity and status, with reassessment where an event changes the basis of the earlier decision.
Derive environmental and substrate-condition records from the product and project requirements. The time and place of a reading matter as well as its value. One observation at the beginning of a shift does not prove that conditions remained unchanged throughout the day. Set the checking frequency through the agreed procedure and characteristics of the work. A process using a polyurethane primer should not inherit automatically completed fields from an unrelated coating form. Adapt the form when the required information differs. Where a measurement cannot be made or suitability remains unresolved, identify the work status explicitly. Leave an honest record of missing information rather than adding an approximate value retrospectively to make the sheet appear complete.
Connect each application record to the coated parts
The application record should identify which materials reached which components. For a prepared mixture, record the product and component batches, preparation time, approved measuring method and receiving parts or areas. Several mixtures may be prepared during a single shift, and distinguishing their destinations can be useful if a later concern requires investigation. Instead of making an uncertain assumption about the whole day's output, the team can identify the relevant group. Follow mixing, induction and thinning requirements through the current product reference in the work order. If an epoxy thinner or another ancillary material is used, include its identity. Small quantities do not make the material irrelevant to traceability or the approved process.
When an unexpected change occurs, record the decision as well as the action. The method may change, a material may become unavailable or application may be interrupted. Note the reason, technical assessment and affected components. A material from another family, such as quick-drying industrial thinner, is not an authorised replacement merely because its general purpose sounds similar. One operator may remember every detail, but that knowledge can disappear at a shift handover. Records allow the process to continue without depending on one person's memory. Clearly separate components subject to a concern so that they do not accidentally advance to the next coat or packaging. Production convenience should not turn an unresolved status into an acceptance label.
Keep the measurement method with the result
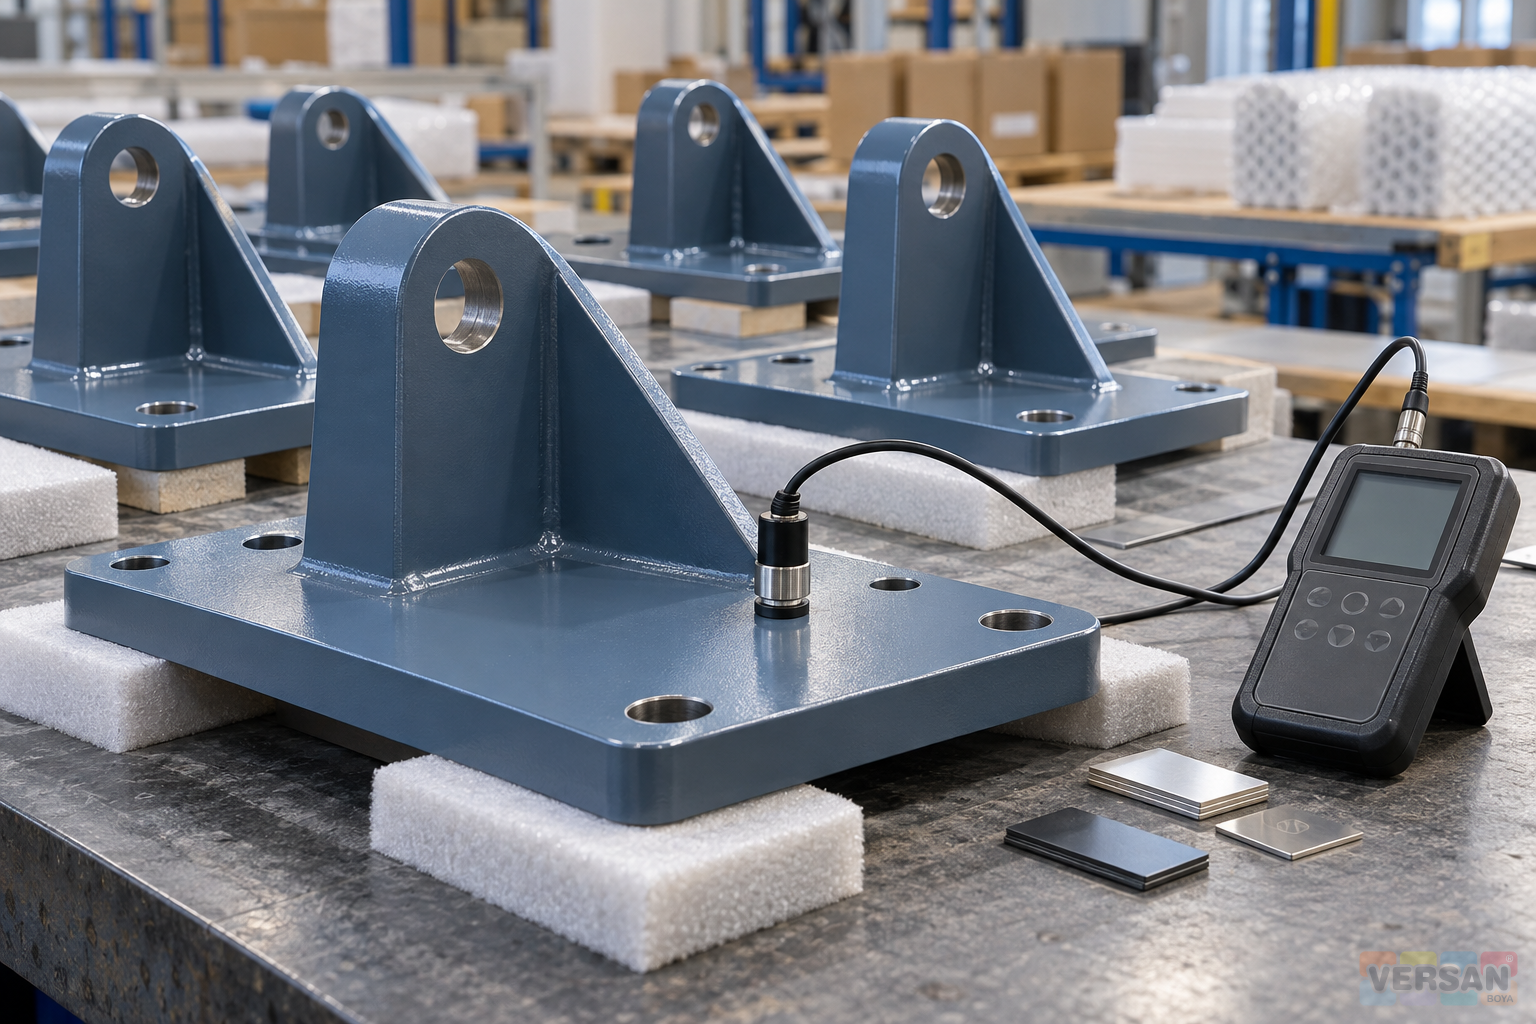
If thickness or another characteristic is measured, the plan needs more than the instrument's name. Define the purpose, suitable method, equipment identity, verification status, sampling arrangement and criterion used to evaluate the result. Elcometer distinguishes calibration performed by the manufacturer or an authorised laboratory from adjustments and checks made by the user before measurement. Preserve that distinction in the record headings. Checking an instrument against a reference on site should not be described as a new laboratory calibration. Follow the equipment instructions and establish suitability for the job. Copying a displayed value into a form is insufficient unless the record also connects it with the correct component, location and valid measurement arrangement.
If unexpected readings occur, do not report only the values that look acceptable. Evaluate the finding using the agreed method and project requirements, retaining the original record when further checks are added. In a system specifying a gloss polyurethane topcoat, numerical measurement still does not replace every acceptance topic. Colour, general appearance, masked areas and other scope requirements may need separate review. Where sampling is used, the record should show which components were selected and on what basis. One acceptable sample does not automatically release an undefined population. The responsible technical person should establish a sampling approach appropriate to the work rather than rely on a universal number of readings copied from an unrelated job.
Manage findings through a recorded closure decision
The value of an inspection plan is not measured only by the number of signatures on acceptable work. Its usefulness becomes clearer when something goes wrong. A nonconformity record should identify the component, observed condition, relevant requirement and temporary status. Then use the authorised route for correction, further assessment, concession or another disposition. A concession is not an informal permission that an applicator grants independently. Authority and scope must be explicit. Determine what needs reinspection after corrective work, and add the closure decision without deleting the original finding. The file then explains how the matter was resolved rather than offering only a final photograph that appears satisfactory. That history can support later improvement of similar work.
An excessively detailed coding system is not always helpful if different teams classify the same finding differently. Use clear descriptions and supporting photographs where appropriate. Do not combine a shortcoming in an antirust primer application and an appearance concern in another system under an unexplained product-failure heading. Preserve the relationship between material, application, substrate and acceptance condition. Repeated findings may justify a separate investigation of causes. The inspection form should not assign blame before the evidence supports a conclusion. Record what was observed first, then add the supported assessment. This sequence also gives production and quality staff a concrete basis for discussing the problem instead of arguing over an assumed explanation.
Release for dispatch involves more than appearance
Before dispatch, establish whether the complete work-order scope has been fulfilled, unresolved findings remain, required records are linked and component identity will survive packaging. Handling and packing readiness must be assessed using the current product instructions and actual conditions. A surface that feels dry is not by itself a sufficient reason to ship. Identify who approves the support, packaging and restraint arrangement. If packing creates new damage, do not make an undocumented touch-up simply because the component was previously accepted. Bring the finding back through the relevant quality process. Connect the dispatch label to the technical acceptance record so that the logistics decision can be traced to the work that was actually released.
If only part of a batch is ready, the dispatch list should show that distinction. Combine physical identification with records to prevent unfinished components from being loaded by mistake. Prepare the handover file around the recipient's needs, using an understandable component list, applicable acceptance records and any open conditions rather than a collection of internal messages. Work specifying a matt industrial finish should not be confused with another batch simply because the colour appears similar. Preserve both product identity and the accepted appearance. Link pre-dispatch photographs to the component or package number. If a later damage report arrives, the team can locate the relevant evidence directly instead of searching through images by date alone.
Carry the plan from first sample into routine work
The first components of a new job provide an opportunity to assess whether the inspection plan can actually be used. Check that required fields can be completed, inspection locations are accessible and responsible people interpret the decisions consistently. Revise the plan when a gap becomes apparent and use the updated version for later production. The first-sample approval guide for industrial coatings discusses this transition. An accepted first sample does not mean all subsequent batches can bypass inspection. Use the sample for the characteristics it was approved to represent. Changes in material, method or scope may require its validity and the inspection plan to be reviewed rather than assumed to continue indefinitely.
A practical plan is only as valuable as its use by the people doing the work. Prefer clear decisions in the correct sequence to a long form whose fields are routinely skipped. Ask which decision each item of information supports. Fields with no useful purpose can be simplified, while material identity, component links, acceptance criteria and authorised decisions remain explicit. When requesting technical support, provide substrate information, production method, service expectations and delivery conditions together. That permits discussion of application and inspection needs alongside product selection. A well-prepared plan is not a guarantee that defects will never occur. It establishes how they can be recognised, their affected scope identified and their resolution closed with evidence.
Test whether another shift can follow the record
One simple internal exercise is to give an authorised colleague the records of a completed job without a verbal explanation. Can that person identify which material was used on each component, which inspections were completed and who permitted dispatch? If not, adding more boxes may be less useful than clarifying identity and decision links. Two accurate mixture records still provide incomplete traceability if neither identifies the receiving group of parts. This is an illustrative process-review exercise, not a claim about a real customer case or a mandatory clause in a standard. Use what it reveals to improve the next form revision, recording why the change was made so that the same ambiguity does not return.
A similar exercise can start at a package number and work backwards through the component list to the acceptance record. If the connection exists only in personal notes, the organisational record is incomplete. Access can remain appropriate to each person's responsibilities; not everyone needs to see every document. However, an authorised person should know where the necessary information is held. This arrangement makes it easier to identify the relevant scope when a concern arises rather than make assumptions about all production. Adapt the final plan to the organisation's real working practices. Clear responsibility, usable records and timely decisions provide a stronger foundation for control from receipt to dispatch than complexity that nobody consistently maintains.