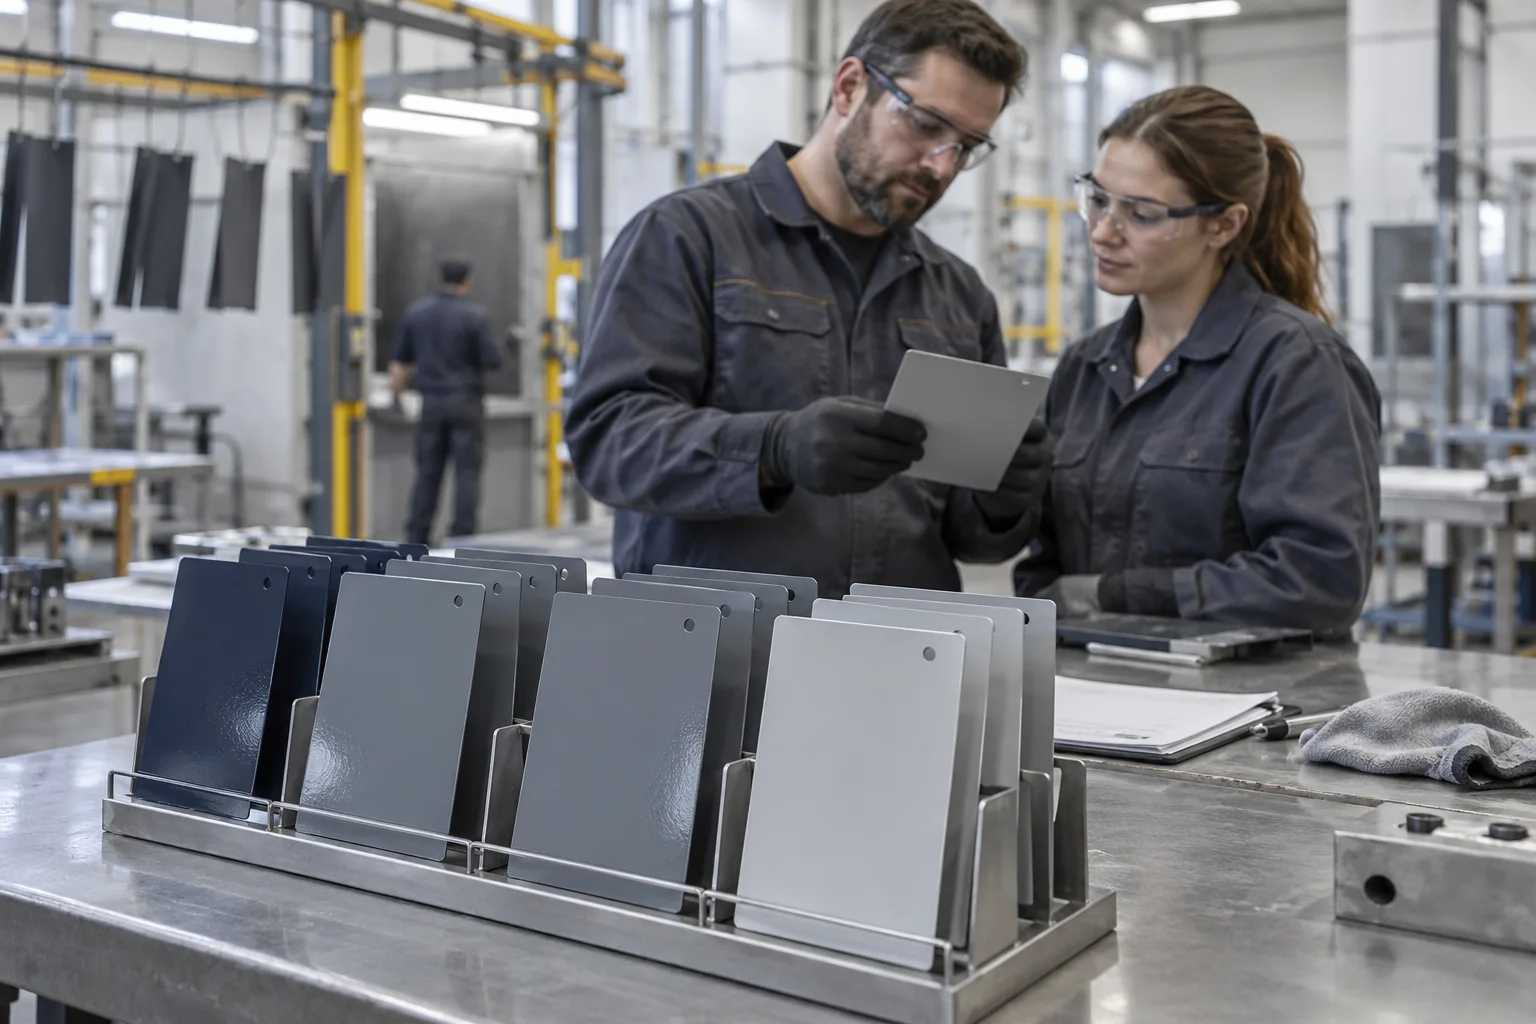
The first coated sample is more than a small panel on which a customer approves a colour. Properly managed, it becomes a shared reference for the selected materials, surface preparation, application method and acceptance expectations. If its purpose is unclear, a signed sample can still leave purchasing, production and inspection teams working to different interpretations. The result may be avoidable rework when full production begins.
First-sample approval should therefore be part of production planning, rather than an inspection exercise added after painting. Technical purchasing, applicators, quality personnel and the customer's decision makers need access to the same information. This guide explains how to connect industrial coating selection with a practical sample and acceptance process. It does not replace a specified test method or project requirement. Product instructions and the agreed specification remain the basis for the work.
1. Define the decision that the sample must support
Start by writing down the questions the sample is intended to answer. Is the purpose to compare colour and gloss, assess preparation, check application on a difficult component, or establish a first-production reference for a complete system? A sample may address several of these purposes, but each needs its own acceptance heading. A panel made for visual assessment should not be presented as proof that every service requirement has been demonstrated.
Describe the approval scope in a short, clear statement. For example, a record might identify the visual assessment of a sample prepared on a specified substrate using a stated method. If system suitability or a particular performance requirement still needs confirmation, list it as an open item. This prevents a signature from appearing to approve something that was never evaluated. It also helps the production team understand exactly what must be repeated and which decisions remain with the technical reviewers.
2. Translate expectations into usable acceptance criteria
Terms such as “excellent finish”, “durable” or “high quality” do not define an inspection decision on their own. Identify where the component will be used, which surfaces will be visible, what imperfections matter and how they will be assessed. If the job requires a defined viewing arrangement, method or reference, agree it before coating begins. Introducing a new criterion only after seeing the result can create an unnecessary dispute between supplier and customer.
Organise requirements under service, appearance, application and documentation. Service covers the actual exposure; appearance covers the required colour, texture and gloss; application covers available equipment and practical conditions; documentation identifies the required product and process records. The steelwork coating specification guide develops this approach for structural steel projects. Review any inspection form inherited from a previous job before reusing it. A familiar document may contain requirements that do not represent the current component or intended service.
3. Use a substrate that represents the real work
The sample's material, surface condition and geometry should relate to production. A flat panel may be convenient for colour assessment, but it cannot fully demonstrate application around edges, welds, openings or restricted areas. In those situations, a flat reference panel and a representative component can serve complementary purposes. Record what each specimen is intended to demonstrate so that a good result on one is not extended beyond its scope.
Document the sample's material supply and preparation history. A new, clean panel will not reproduce all the uncertainties involved in coating a previously painted maintenance surface. Similarly, a result obtained under laboratory conditions may depend on equipment or controls unavailable on the production floor. Ask whether the process can be repeated on actual parts, at the intended scale and within the real work sequence. That question turns sample making from a presentation exercise into a useful production decision.
4. Identify materials at product and component level
A generic coating-family name is insufficient for a traceable sample record. For each selection from the coating product catalogue, record the full product name, code, relevant components and associated documentation. Where a product has application options, identify the option used for the sample. Linking purchased material to the sample record makes the later transition to a production order much easier to control.
When considering an epoxy primer and an epoxy topcoat, confirm the combination for the actual substrate and service. A common brand name does not establish universal compatibility or suitability. Connect each document in the sample file to the relevant product code. If the available record does not provide an issue date or revision, do not invent one. Track any requirement for updated confirmation as an open technical item.
5. Compare alternatives against the same requirement
Before evaluating an alternative product, explain which requirement is driving the change. A shorter process window, different appearance, compatibility with existing equipment or another service condition may each require a different assessment. For instance, a quick-drying industrial paint should not be treated as equivalent to another system solely because of an anticipated drying advantage. Compare verified product scope with the project requirements, not just one attractive characteristic.
Likewise, the name gloss polyurethane topcoat does not establish suitability for every metal or timber application. The relevant catalogue record on this site describes furniture substrates; another substrate or coating combination requires product-specific confirmation. A successful-looking sample does not remove that documentation question. The broader epoxy, polyurethane and acrylic selection guide provides additional context for discussing system families while preserving the distinction between a general comparison and an approved product specification.
6. Record the preparation that will later be hidden
Once the sample is coated, much of its preparation is no longer visible. Record the preparation sequence, accepted surface condition and final inspection before applying the coating. Where preparation and application are handled by different people, the handover check is especially useful. Waiting time, transport and temporary protection also form part of the sample's history. A completed finish cannot retrospectively demonstrate every condition that existed underneath it.
A change in preparation equipment or materials may require review. That does not mean every change produces a poor result; it means the same process should no longer be assumed without consideration. Record who accepted the prepared surface and on what basis. This approach moves quality control away from simply looking for defects at the end. It establishes appropriate checks at the stages where the relevant evidence can still be seen and where a correction can be made before more work is added.
7. Keep the application record practical
A complicated form can become a form that nobody completes properly. Use concise fields for the information needed to reproduce and assess the sample: product and batch, quantity prepared, component identification, mixing time, application method, start and finish, environmental and substrate conditions, and release to the next stage. Obtain numerical requirements from the relevant product instructions. Do not populate every product record with one assumed mixing ratio or waiting period.
Record the selection and quantity of thinners and auxiliary materials separately. “Thinned as required” provides little help when comparing the sample with later production. Clear identification makes process differences easier to investigate. Leave a short space for operator observations as well. A difficulty involving flow, coverage or access may influence production even when it is not obvious in the final appearance. Record unknowns honestly rather than turning an unmeasured condition into an apparently precise value.
8. Assess appearance under consistent conditions
Agree a common arrangement for colour and appearance review instead of comparing the sample informally in several unrelated environments. Reference-panel condition, lighting and the timing of assessment can all affect how useful the comparison is. Photographs are valuable documentation, but a phone image or screen display should not automatically replace the agreed physical reference. State what the acceptance decision was actually based on.
If visible faces and normally concealed areas have different requirements, distinguish them clearly. Discuss expectations at edges, joints and restricted areas before application rather than after the sample is finished. The technical coatings glossary can help teams use terms such as gloss, matt appearance and hiding consistently. When a term remains ambiguous, define an assessment method or reference instead of adding more adjectives. Practical clarity is more useful than wording that sounds precise but cannot support a repeatable decision.
9. Plan measurements for the component geometry
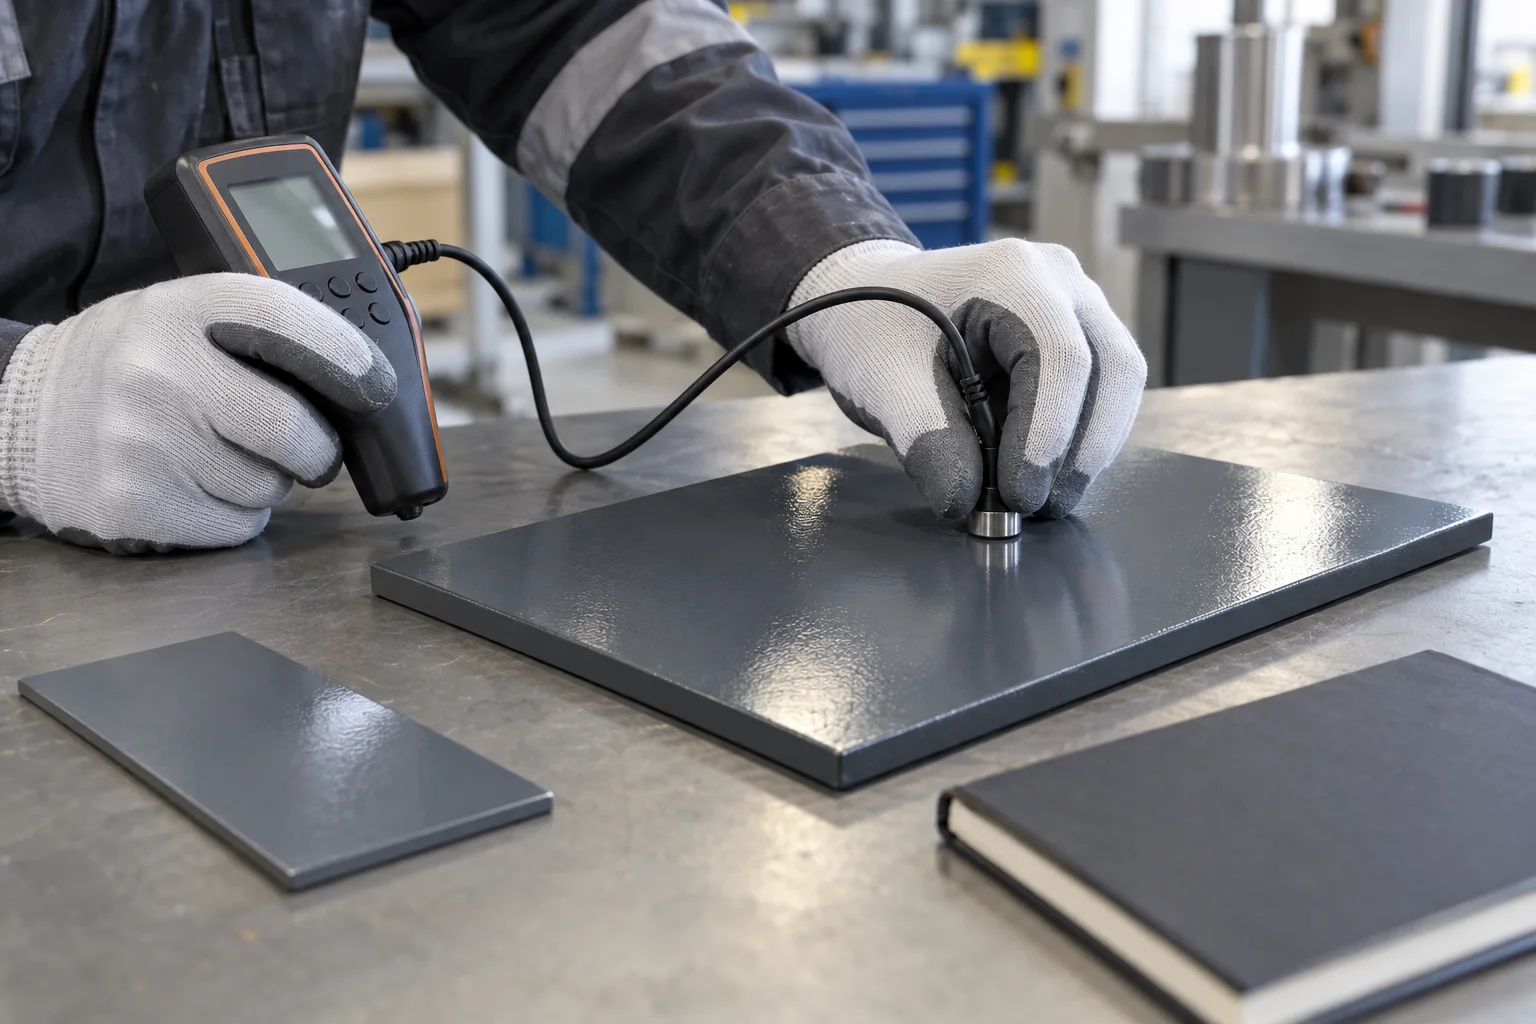
Do not select inspection locations only because they are easy for the instrument to reach. Consider the geometry and access conditions when deciding which areas need assessment and how the selected method applies. For film-thickness measurements, for example, instrument suitability and verification matter alongside the readings. A number on a display does not, by itself, demonstrate that the measurement is valid under every surface condition.
Agree the inspection plan and acceptance basis before reviewing the results. They should follow the relevant product instructions, project specification and chosen method. A special service-performance requirement or certification need must remain distinct from the scope of a workshop sample. Where a check is destructive, include the subsequent repair or replacement of the sample in the plan. Knowing why each measurement is being taken avoids collecting a large quantity of data that does not resolve the actual approval question.
10. Separate drying, handling and release to service
A sample that appears ready to touch is not automatically ready for stacking, wrapping, assembly or service exposure. Each transition should follow the requirements of the selected product and the conditions actually achieved. Samples made on the same day may have different histories if they were held in different locations. Contact with labels, supports, packing materials or adjacent components can also be relevant to the record.
Arrange coating, waiting, inspection and dispatch so that the production schedule does not force an undocumented technical shortcut. A short delivery window does not change the product requirements. If the intended production rate and selected system are poorly matched, discovering that during sampling is useful. Phasing or another technically suitable approach may need consideration. An option should not be labelled approved merely because it fits the calendar; it still needs the appropriate product and process evaluation.
11. Distinguish approval, conditional approval and rejection
An approval record should identify the specimen, the supporting records and the exact scope accepted. A simple “approved” stamp may leave too much open to interpretation. If appearance is accepted but technical confirmations remain outstanding, record a conditional decision and list those items. Assign responsibility for closing them and identify the evidence needed. Otherwise, a conditional approval can easily circulate through production as if it were unrestricted.
When rejecting a sample, identify the unmet criterion and observed condition, rather than writing only that the finish was not liked. State what needs to change before the next trial. Changing several variables at once can make the reason for a different outcome difficult to understand. Maintain the link between revisions and preserve earlier records. Both successful and unsuccessful trials become useful organisational knowledge when their purpose, changes and outcomes can be followed.
12. Transfer the approved process into production
Make the approved physical reference, or an appropriately identified counterpart, accessible to production and quality teams. Link the product codes, document versions and application plan to the same file. A purchase order containing only a generic paint name can break the connection between the material sampled and the material supplied for the job. Checking the order against the technical file is a straightforward way to reduce that uncertainty.
Review the first production components against the approved reference and process records. This helps identify differences introduced by the change in scale, equipment, operator, substrate or work sequence. A seemingly small change should be considered rather than automatically dismissed. Record whether a further trial or review is required and why. Nobody should have to rely on a remembered conversation as the only authority for changing a material or method.
13. Include the sample information in the enquiry
Provide sample scope, accepted options and outstanding technical matters alongside the component quantity or surface area. Identify packaging preferences, colour requirements, batch traceability and delivery stages. Compare quotations for the same work scope rather than reducing different systems to a price per kilogram. The industrial coating procurement and technical enquiry guide explains how to connect technical information with a more useful purchasing comparison.
Use the coating quotation request form to identify products and packaging, and describe the intended application in the enquiry. Keep the sample reference and supporting file available for the technical discussion. Where product scope, documentation or system suitability remains uncertain, contact Versan Boya for a technical review using the exact product code. A complete enquiry helps prevent different participants from pricing or approving different interpretations of the same job.
14. Define which changes trigger a review
An approved sample is a reference to a defined set of conditions, not a permanent permission to change anything around it. Establish a short change-review list that suits the project. A different substrate supplier, another preparation method, a changed coating component or a new application arrangement may need assessment. The list should help staff recognise when to ask for review without making routine work unnecessarily complicated.
The review should record the change, its relevance to the acceptance scope and the evidence used to decide whether another sample is necessary. Keep the original reference identifiable even if a revised one replaces it. This is particularly useful when several teams or sites work on the same order. A controlled revision prevents two different specimens from both being described informally as “the approved sample”.
Final checks before production release
- Is the sample purpose and represented service clearly recorded?
- Do the substrate, preparation, product codes and components match the intended work?
- Are unknown application or holding conditions explicitly identified?
- Are visual approval and other technical requirements distinguished?
- Are inspection methods, equipment suitability and measurement locations traceable?
- Have open conditions been communicated to the production team?
- Are the physical reference, document version and ordered products connected?
- Is responsibility for reviewing later changes clear?
The same amount of paperwork is not appropriate for every project. A small maintenance component and a large production order may justify different levels of documentation. In both cases, however, the material used, the decision basis and the process to be repeated should be understandable. Good sampling reduces uncertainty rather than simply generating forms. The file becomes useful when each participant can answer the essential questions from the same reliable record.
Sources and technical scope
Product descriptions were checked against the site's Nanomix records and available technical catalogue documents. The different application descriptions of epoxy and polyurethane products have been preserved; one product's numerical application values have not been transferred to another. A sample is not automatic certification of special service performance or an entire production batch. Follow the selected product's current instructions and the agreed project requirements. Images are representative editorial scenes of sample review and coating inspection.